What Are Welding Parts and How Do They Work?
Welding Parts are the components that make a welded assembly possible and dependable. They include base metals, prepared joint edges, filler metal, and, in many applications, brackets or fittings. Their job is not simply to meet at an arc. Each part must fit, carry load, and tolerate the heat introduced during welding. A small gap at a pipe joint or a misaligned bracket can change penetration, strength, and appearance. Details matter.
The American Welding Society’s 2023 workforce data projected that the United States would need about 360,000 welding professionals by 2027. That estimate reflects welding’s continuing role across manufacturing, construction, transportation, and repair. It is not a parts-quality measure, but it shows why clear technical knowledge matters. Welding educator Larry Jeffus’s teaching emphasizes preparation and process control; a useful paraphrase is, “The weld begins before the arc.” This is a paraphrase, not a verified verbatim quotation.
This guide explains how Welding Parts work together, from joint design and fit-up to filler selection and heat control. It also considers how material thickness, surface condition, and alignment affect the finished connection. A clean edge and a steady fit can be more important than they look. Still, no single checklist guarantees a sound weld; inspection and skilled judgment remain essential. Understanding these fundamentals helps readers ask better questions, spot avoidable problems, and make more informed fabrication decisions.
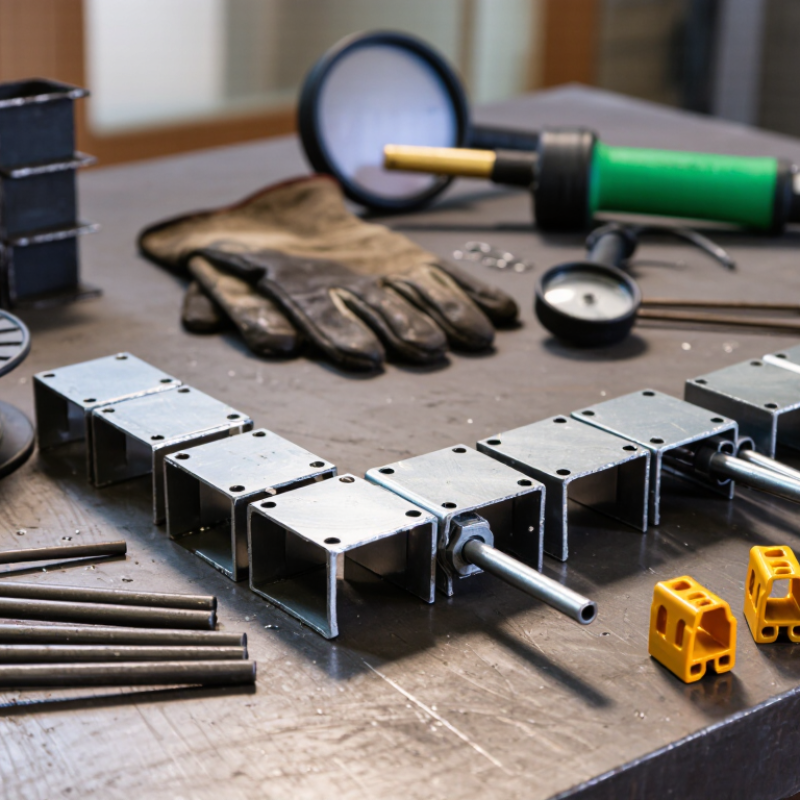
Table of Contents [Hide]
What Welding Parts Are and Their Role in an Assembly
Welding parts are separate metal components intended to become one assembly through welded joints. They may be plates, tubes, brackets, frames, or small tabs that locate and support other pieces. Their shape and thickness affect joint design, torch access, and heat flow. In a practical assembly, a bracket can transfer load into a frame, while a short gusset helps resist bending. Small details matter.
Before welding, parts are positioned to meet specified gaps and alignment; clamps or fixtures hold them while tack welds limit movement. The joint transfers force across the fused area, but performance also depends on material compatibility, weld size, penetration, and workmanship. Heat can pull a long panel out of square, so fit-up and welding sequence deserve attention. Not every seam needs the same treatment. A drawing may call for a continuous weld in one location and intermittent welds elsewhere, depending on loading, sealing, and design requirements. After welding, visual checks can reveal undercut, cracks, or uneven bead shape, while critical joints may need additional inspection. Real assemblies are rarely perfect on paper. A small gap may be unavoidable, but it should be assessed against the drawing and approved welding procedure, not simply hidden under extra weld metal.
What Are Welding Parts and How Do They Work? - What Welding Parts Are and Their Role in an Assembly
| Part or Feature | What It Is | Role in an Assembly | How It Works | Typical Examples or Notes |
|---|---|---|---|---|
| Base metal | The parent material or components being joined. | Forms the main structure and carries the loads specified for the assembly. | The edges are heated until they melt or become suitable for joining; filler metal may also be added. | Common materials include carbon steel, stainless steel, aluminum, and nickel alloys. |
| Weld joint | The arrangement where two or more components meet for joining. | Sets the connection geometry and affects access, strength, and weld preparation. | The parts are positioned in a configuration such as a butt, lap, tee, corner, or edge joint, then welded as specified. | Joint type and preparation depend on the design, material thickness, loading, and applicable requirements. |
| Filler metal | Consumable metal added to the weld in processes that use filler. | Fills the joint gap and contributes metal to the completed weld. | It melts during welding and fuses with the prepared joint and, where applicable, the base metal. | Supplied in forms such as wire, rod, or covered electrodes; selection should suit the base materials and procedure. |
| Weld metal and weld bead | Weld metal is the fused material; the weld bead is the visible deposit formed along the joint. | Creates the metal connection between components. | The molten pool cools and solidifies into a continuous or specified sequence of weld passes. | Bead size, shape, and number of passes are determined by the joint design and welding procedure. |
| Heat-affected zone (HAZ) | The area of base metal next to the weld that was heated but did not melt. | Remains part of the assembly and can influence the properties of the welded area. | The welding heat cycle can change the material’s microstructure or mechanical properties in this region. | Its size and properties vary with material, heat input, thickness, and cooling conditions. |
| Backing bar or backing material | A support placed behind a joint root when the welding procedure calls for it. | Supports the weld pool and can help achieve the required root profile. | It provides a surface beneath the joint during welding; it may be retained or removed depending on the design. | Backing can be metallic or nonmetallic and must be compatible with the specified procedure and service conditions. |
| Tack weld | A short, temporary weld used to hold components in position before final welding. | Helps maintain alignment and joint fit-up during assembly and welding. | Small welds are placed at selected points; they may be incorporated into or removed before the final weld as required. | Tack welds should be suitable for the material and procedure and should not contain defects that compromise the final weld. |